PROEXPORT / INDUSTRIAL ROLLERS
Plasma-Sprayed Ceramic Rollers | PROEXPORT
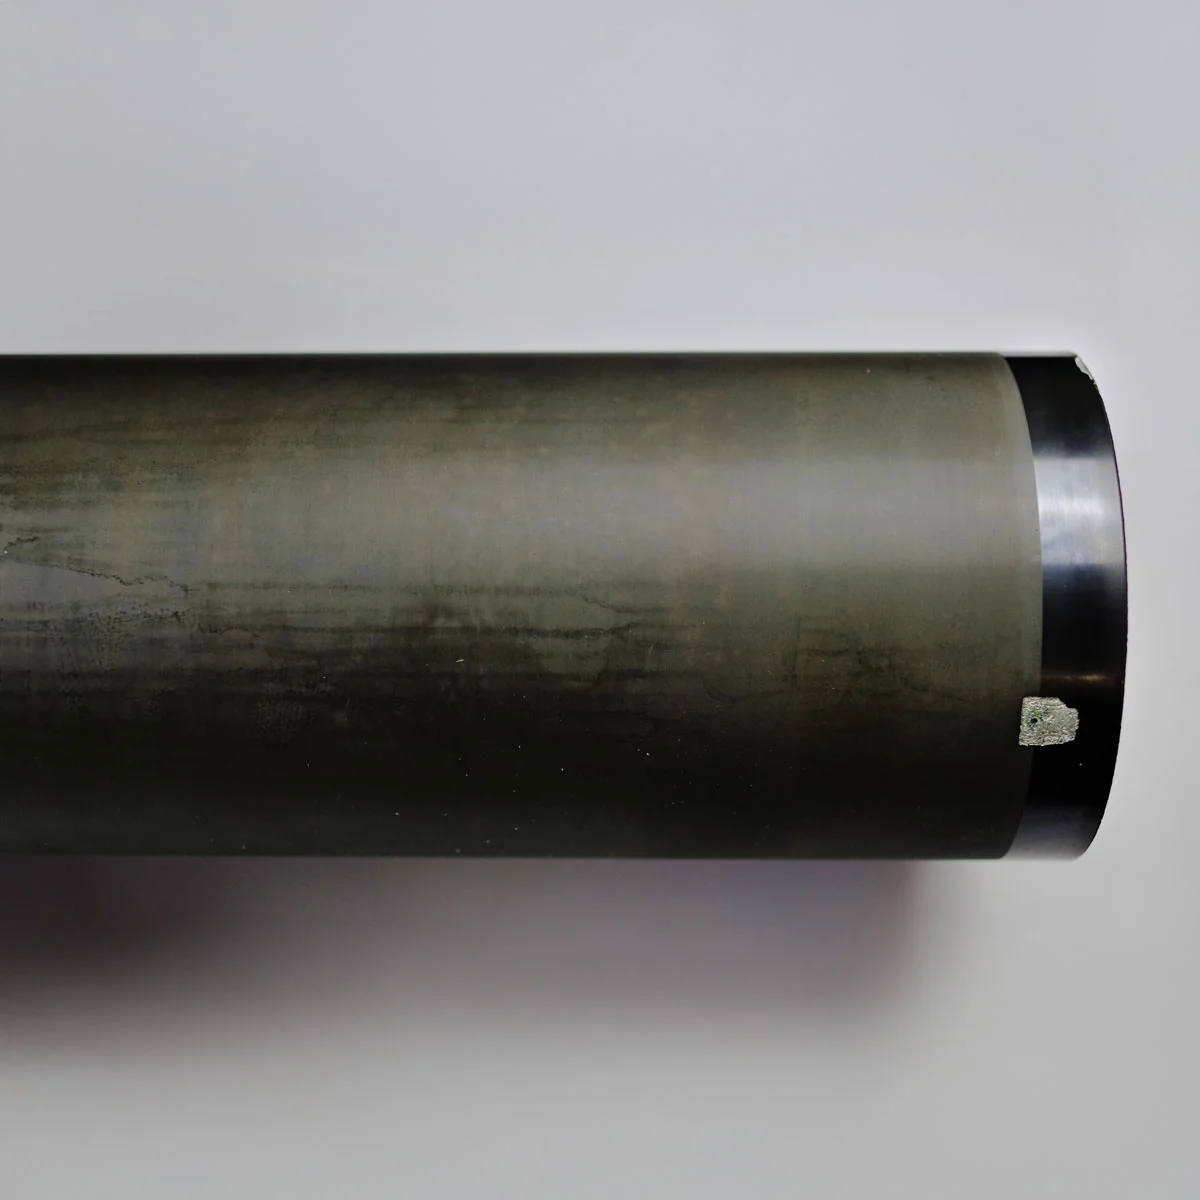
PROEXPORT plasma-sprayed ceramic rollers feature advanced thermal-spray coatings of chromium oxide (Cr2O3) or alumina-titania (Al2O3-TiO2) delivering extreme micro-hardness up to 1400 HV. They are engineered for abrasive converting, web corona treatment, corrosive chemical environments, and applications where metallic rolls fail prematurely.
TECHNICAL SPECIFICATIONS
Manufacturing Parameters and Operating Tolerances
We match core construction, elastomer compound or metallic coating, and surface finish directly to the operating conditions on your line.
| Technical Parameter | Specification / PROEXPORT Standard |
|---|---|
| Coating Material | Cr2O3 (Chromium Oxide) / Al2O3-TiO2 (Alumina Titania) plasma thermal spray |
| Coating Hardness | 1200 to 1400 HV (approx. 72 to 75 HRC equivalent) |
| Layer Porosity | < 1.5% with high-temperature polymer or fluoropolymer pore sealing |
| Surface Finish | Diamond-ground finish from Ra 0.1 µm to Ra 1.2 µm |
| Max Dimensions | Diameter up to Ø1000 mm, overall length up to 4000 mm |
| Dielectric Properties | High electrical breakdown resistance for corona treatment rolls |
LINE PROBLEM SOLVING (PWE)
Precision that Eliminates Line Downtime and Web Defects
At PROEXPORT, we do not simply supply coatings — we solve specific engineering challenges for plant technologists and maintenance leaders.
PRODUCTION CHALLENGE
Line Issue
Severe abrasive wear, pitting, and chemical attack rapidly destroying metallic roller surfaces and doctor blades.
PROEXPORT SOLUTION
Engineering Solution
Dense plasma-sprayed ceramic barrier coating sealed against chemical penetration and finished with diamond grinding wheels.
PLANT ROI RESULT
Measurable Effect
5x longer service life compared to hard chrome in abrasive environments, zero chemical corrosion, and stable line friction.
SELECTION & QUALITY CONTROL
Pre-Production Specification & Quality Inspection
Every project — new fabrication or reconditioning — is executed according to strictly defined inspection points:
- Cross-sectional coating micro-hardness testing (HV 0.3).
- High-voltage dielectric spark testing for corona treaters.
- Surface roughness Ra and Rz verification with diamond-tipped profilometers.
- 100% dye penetrant and ultrasonic bond integrity inspection.
Technical Acceptance Standards
| Inspection Dimension | Technical Significance |
|---|---|
| Geometry & Tolerances | Diameter calibration, radial/axial runout, and concentricity of bearing journals. |
| Coating Structure | Durometer Shore/HV verification, nominal thickness, and zero-porosity bonding. |
| Dynamic Balancing | Residual unbalance compensation in ISO 1940 Grade G 2.5 or G 6.3. |
FREQUENTLY ASKED QUESTIONS (FAQ)
Frequently Asked Questions (FAQ)
When should ceramic coating be chosen instead of hard chrome?
Ceramic coatings are selected when operating in highly abrasive slurry, doctor blade contact, strong acids/chlorides, or high-voltage dielectric corona applications where hard chrome wears or delaminates.
Can ceramic rollers withstand mechanical impact?
While ceramics have unmatched hardness and abrasion resistance, they are brittle. Point impacts must be avoided, and thermal expansion matching with the metal core is accounted for in our design.
PROEXPORT / INDUSTRIAL ROLLERS
From technical drawing to line-ready solution.
Submit dimensions, photos, and operating conditions. We will determine the optimal manufacturing or reconditioning scope.